
Air Handling Units (AHU)
In addition to industrial finned coils, Advanced Coil can incorporate our heat exchanger designs into custom-engineered, heavy-duty, industrial air handling units. Our stripped-down AHUs are the perfect fit for industrial process heating or cooling.


Air Handler Unit Construction
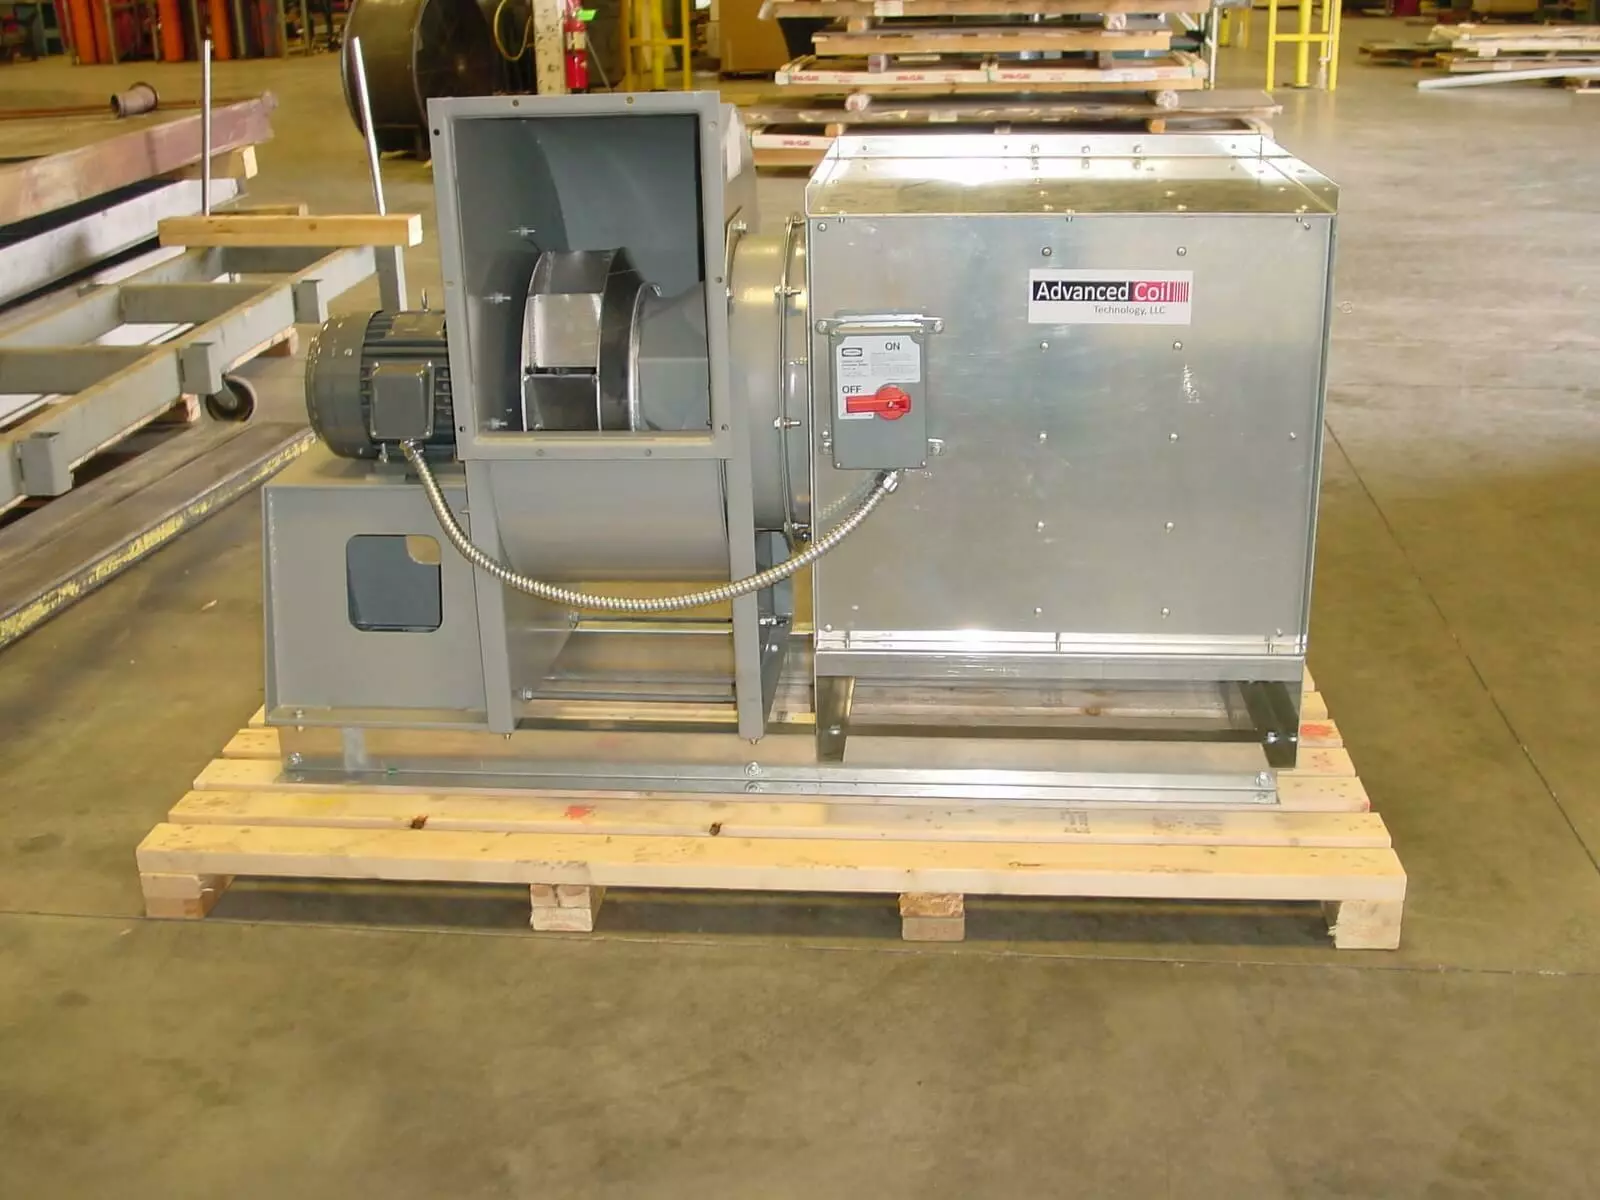
The construction of an industrial process air handler unit (AHU) incorporates numerous components—such as fans, heat exchangers (typically chilled-water, hot-water, or steam), filters, and dampers—contained within a metal housing.
Advanced Coil manufactures AHUs using high-quality, corrosion-resistant materials, including stainless steel heat exchange tubing, aluminum fins, and galvanized steel casings and housings. Where required, we also integrate stainless steel components to enhance durability in harsh or sanitary environments.
For thermal and acoustic insulation, we commonly use fiberglass or mineral wool, providing reliable performance and long-term protection against temperature loss and noise transmission.
We can also manufacture custom components, such as:
- Return and makeup air units
- Face & bypass units
- Filtration: 30% roughing filters to HEPA filters
- Blowers and fans
- Dampers
- Access doors and panels
Packaging these components together into complete AHU systems supplies you with a higher quality single-source product that reduces the costs associated with assembling and installing separate components from multiple suppliers on your job site.

Durable. Reliable. Proven.
Our 5-Year warranty demonstrates our products are engineered to perform and built to last. Since 1995 we have stood behind our work. Durable. Reliable. Proven. Ultimately, this is about your peace of mind.
We Can Certify our AHUs According to the Following Standards:
- ASME
- National Board registration
- CRN registration
- We can also U-stamp any pressure-vessel-type heat exchangers or high-pressure steam or hot water coils.
Design Benefits
A well-designed AHU maximizes airflow with minimal resistance, reduces energy losses, and optimizes coil heat transfer. Influencing factors include fan configuration, heat exchanger arrangement, damper placement, and insulation quality. Furthermore, thoughtful considerations like sloped, stainless steel cooling coil drip pans can extend an AHU’s lifespan and reduce maintenance requirements.
AHU Industry Applications
An AHU’s primary purpose is to provide ventilation, control air temperature and humidity, and filter out airborne particles. Several typical applications include:
- Food Processing Facilities: Preventing contamination by managing humidity
- Industrial HVAC Systems: Ensuring worker comfort and optimizing production machinery operation by providing air conditioning
- Power Plants: Keeping control room equipment at a stable temperature with air conditioning
- In addition, AHUs can be found in warehouses, mezzanine platforms, and indoor agricultural cultivation facilities.
AHUs Backed by Advanced Coil’s 5-Year Warranty
At Advanced Coil, we manufacture our air handling units for optimal performance and durability. Along with features such as press-fit fans and unexpanded tubes and techniques like TIG welding, this allows us to offer a 5-year warranty, the longest standard warranty period in our field. Contact us today to request a quote on your custom-engineered AHU.
Additional Products We Offer


Have Questions?
Give us a call or fill out the form and one of our team members will be in touch as soon as possible.
507-451-0130


