
Airtight Coil & Heat Exchanger Housings
Advanced Coil is dedicated exclusively to the design and manufacture of heavy-duty, custom heat exchangers for industrial and process applications. Our goal is to deliver a complete, tailored solution—from engineering through fabrication—to ensure long-term performance and reliability.
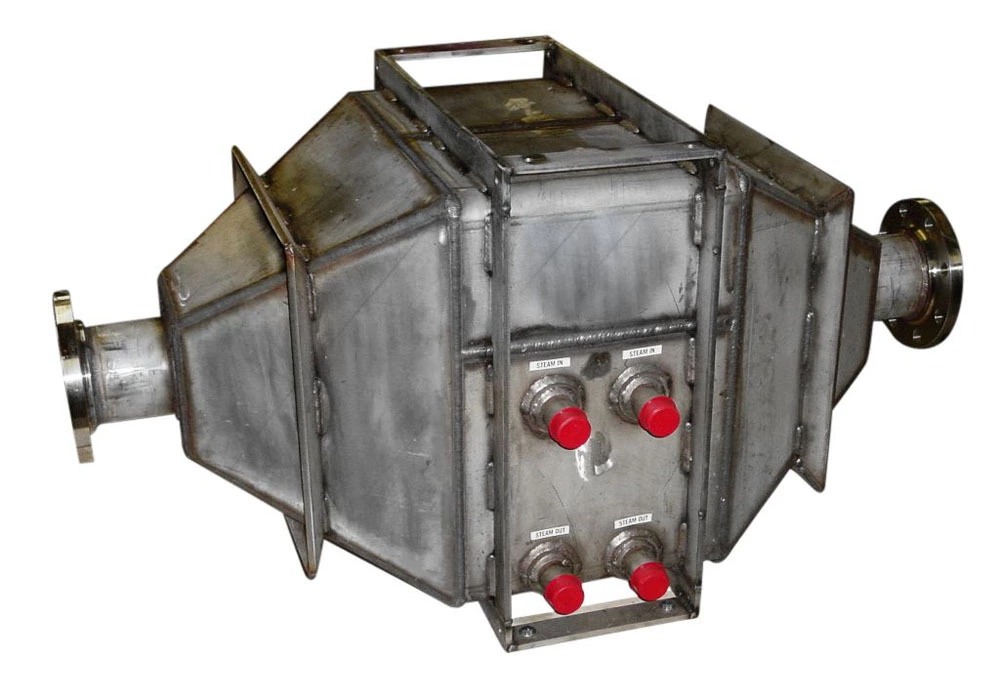
Our airtight coil housings are engineered to eliminate cross-contamination between the process airstream and the surrounding environment, ensuring system safety, efficiency, and optimal heat transfer performance.


Airtight Heat Exchanger Housing Design and Benefits
The structural design of our airtight coil housings incorporates robust sealing features—including gaskets, precision seals, and TIG-welded joints—engineered to handle operating pressures from full vacuum to 100 psig. Many designs also include flanged, bolted connections to ensure proper gasket compression and long-term leak-free performance. To accommodate thermal cycling, we integrate expansion joints that absorb movement caused by temperature fluctuations, protecting the housing and maintaining airtight integrity under demanding process conditions.
Some of Our Optional Features Include:
- Inspection and access panels
- Drip pans for condensate or cleaning solution
- Structural legs
- Custom mounting configurations
- Lifting and installation brackets
- Support structures
- Face and bypass dampers
- Integrated filter sections
Standard Materials
We use durable and corrosion-resistant construction materials depending on your application’s requirements:
- Galvanized Steel: 12 gauge to 7 gauge
- Painted Steel: 12 gauge to 7 gauge
- 304L Stainless Steel: 12 gauge to 3/8" thick
- 316L Stainless Steel: 12 gauge to 3/8" thick
If you have a highly specialized application, our experts will work with you to choose the materials best suited for your process.
Industrial Applications for Slide-Out Coil Housings
- Food and Meat Processing Plants – Smokehouses, ovens, and RTE (ready-to-eat) facilities where coils must be cleaned regularly to maintain sanitation and prevent contamination.
- Powder and Ingredient Manufacturing – Drying and blending systems where airborne particulates can accumulate on coils, increasing the risk of buildup or combustion.
- Chemical Processing Facilities – Heat exchangers handling corrosive or reactive vapors that require periodic cleaning to maintain performance and safety.
- Pharmaceutical Production – Controlled-environment systems where maintaining strict temperature and cleanliness standards is critical.
- Grain and Seed Processing – Heating, cooling, or drying systems where dust and chaff can clog fins or restrict airflow.
- Pulp and Paper Plants – Ventilation or drying systems exposed to high humidity and fibrous material that can settle on coil surfaces.
- Industrial Ovens and Dryers – High-temperature or contaminated airstream applications where removable coils simplify maintenance and extend service life.

Durable. Reliable. Proven.
Our 5-Year warranty demonstrates our products are engineered to perform and built to last. Since 1995 we have stood behind our work. Durable. Reliable. Proven. Ultimately, this is about your peace of mind.
Have Questions?
Give us a call or fill out the form and one of our team members will be in touch as soon as possible.
507-451-0130


